The challenge isn't finding anti-static yarn-it's finding the right one for your specific industrial needs. With surface resistivity ratings, blend ratios, and durability claims varying wildly across suppliers, how do you make an informed decision? This guide walks you through the critical factors that separate genuinely protective workwear from expensive fabric that fails when it matters most.
Understanding Surface Resistivity Requirements by Industry
Surface resistivity determines how quickly electrical charges dissipate through fabric. This measurement, expressed in ohms (Ω), directly impacts whether your work-wear meets industry safety standards.
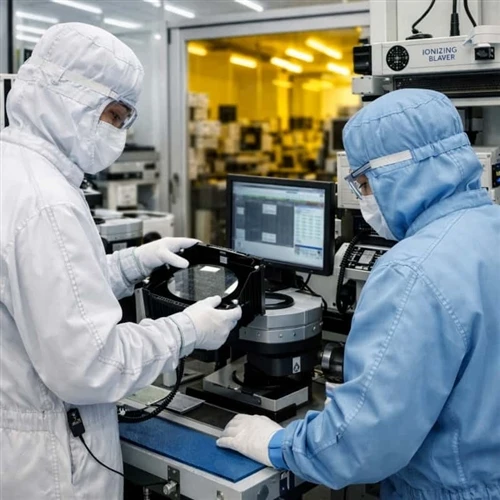
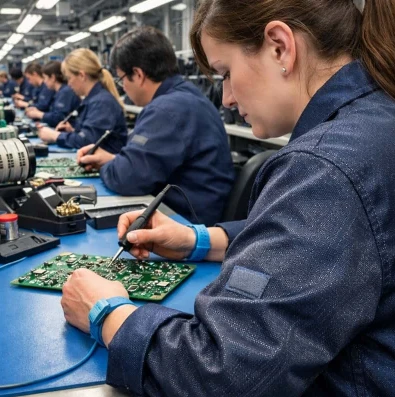
Electronics manufacturing facilities typically require surface resistivity between 10⁴ and 10⁶ ohms. At this level, static charges dissipate in under 0.1 seconds-fast enough to prevent damage to sensitive components like microchips and circuit boards. carbon black conductive yarn achieves this performance through permanent electron conduction, not temporary surface treatments that wash away.
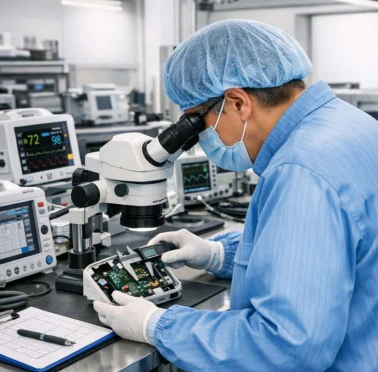
Pharmaceutical cleanrooms operate under different constraints. Here, you need anti-static protection that doesn't compromise sterility. Surface resistivity between 10⁵ and 10⁷ ohms provides adequate static control while maintaining fabric breathability. The key consideration becomes was hability-pharmaceutical workwear undergoes industrial laundering cycles that would destroy coating-based anti-static treatments within weeks.
Petrochemical environments present the highest stakes. Static discharge near flammable vapors creates explosion risks. These facilities demand surface resistivity below 10⁶ ohms combined with proven durability under harsh conditions. The yarn must maintain consistent performance despite exposure to oils, solvents, and extreme temperatures.
Permanent Conductivity vs Temporary Treatments
The anti-static yarn market splits into two fundamentally different approaches: intrinsic conductivity and applied coatings. Understanding this distinction prevents costly mistakes.
Coated anti-static fabrics rely on chemical treatments applied to conventional fibers. These treatments typically last 20-50 industrial wash cycles before performance degrades. Surface resistivity measurements might look impressive initially, but they climb steadily with each laundering. By month three, you're replacing work-wear that no longer meets safety standards.
Conductive yarn achieves anti-static properties through material composition, not surface chemistry. Carbon black conductive fibers blended with polyester create permanent electron pathways throughout the fabric structure. After 500 wash cycles, surface resistivity remains virtually unchanged. The conductive properties can't wash out because they're built into the yarn itself.
This difference becomes critical when calculating total cost of ownership. A garment using 20% carbon black conductive fiber conductive yarn costs approximately 40% more upfront than coated alternatives. However, it lasts 10 times longer while maintaining consistent protection. Over a three-year period, the conductive yarn option costs 60% less per garment while eliminating the compliance risks associated with degraded anti-static performance.
Matching Blend Ratios to Protection Levels
Conductive yarn comes in different blend ratios, each optimized for specific protection requirements. Choosing the wrong ratio either overpays for unnecessary performance or leaves workers inadequately protected.
High Protection Environments: Electronics assembly, semiconductor manufacturing, and precision instrument handling require 40% conductive fiber (CF ) blended with 60% polyester. This ratio provides surface resistivity around 10⁴ ohms with electromagnetic interference (EMI) shielding capabilities. The higher metal content creates more electron pathways, enabling instant charge dissipation. These yarns typically come in Ne21s through Ne50s specifications, with finer counts offering better fabric hand feel.
Medium Protection Environments: Medical equipment operation rooms, pharmaceutical packaging areas, and data centers function well with 30% conductive fiber and 70% polyester blends. Surface resistivity ranges from 10⁵ to 10⁶ ohms-adequate for preventing static damage while maintaining superior comfort and breathability. The lower metal content reduces fabric weight and improves drape, making these garments more comfortable for extended wear.
Basic Protection Environments: General electronics assembly, warehouse operations near sensitive equipment, and standard cleanrooms need only 20% conductive fiber with 80% polyester. This economical option delivers surface resistivity around 10⁶ to 10⁷ ohms. Static charges dissipate within 0.5 seconds, meeting most industrial anti-static requirements without the premium cost of higher blend ratios.
Evaluating Durability and Washability Claims
Supplier claims about durability mean nothing without standardized testing data. When evaluating anti-static yarn options, demand specific performance metrics.
Wash cycle retention tells you how many industrial launderings the yarn withstands before anti-static properties degrade by 20%. Quality carbon black conductive yarn maintains performance beyond 300 cycles. Anything claiming fewer than 200 cycles probably uses coating technology rather than intrinsic conductivity.

Abrasion resistance matters in industrial settings where workers encounter rough surfaces, machinery, and frequent movement. Conductive yarns incorporating carbon black conductive fibers demonstrate exceptional durability because the metal component resists wear. Fabrics maintain structural integrity and anti-static performance even after significant abrasion that would destroy conventional textiles.
Chemical resistance becomes critical in petrochemical, pharmaceutical, and manufacturing environments. Carbon black conductive yarn withstands exposure to acids, alkalis, oils, and organic solvents without performance degradation.
Your Next Steps
Selecting anti-static yarn for industrial workwear requires matching technical specifications to your specific operational requirements. Start by documenting your industry's surface resistivity standards, then evaluate yarn options that meet those thresholds through intrinsic conductivity rather than temporary treatments.
Request sample packs from suppliers offering stainless steel conductive yarn in multiple blend ratios. Test these samples in your actual work environment, measuring both initial performance and durability after multiple wash cycles. The investment in proper testing prevents the far greater cost of deploying inadequate protection across your workforce.
Ready to evaluate anti-static yarn options for your specific application? Contact us for technical specification sheets and sample packs tailored to your industry requirements.
FAQ
Q:
A: What surface resistivity is required for electronics manufacturing work-wear? A: Electronics manufacturing typically requires surface resistivity between 10⁴ and 10⁶ ohms, achieved through 30% carbon black fiber conductive yarn blends.
Q:
A: How long does anti-static yarn maintain its protective properties? A: Carbon black conductive yarn maintains anti-static performance for 300+ industrial wash cycles, while coated treatments typically degrade after 20-50 cycles.
Q:
A: What's the difference between 20% and 30% conductive fiber blends? A: 30% blends provide EMI shielding and faster static dissipation (10⁴ ohms) for high-sensitivity environments, while 20% blends offer basic anti-static protection (10⁶-10⁷ ohms) for general industrial use.
Q:
A: Can anti-static yarn withstand chemical exposure? A: Yes, carbon black conductive yarn resists acids, alkalis, oils, and organic solvents without performance degradation due to the corrosion-resistant properties of stainless steel.